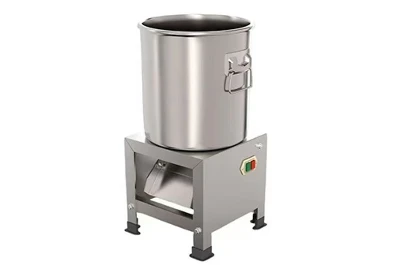

How to Size kg/h Output to Your Herd, Material and Power Supply - Without Buying Twice
A technical sizing guide for importers, distributors and farm operators | 2026 Edition
Feed Chopper Capacity Planning (2026): How to Size kg/h Output to Your Herd, Material and Power Supply
Ask five suppliers for a feed chopper quotation and you will receive five capacity figures: 300 kg/h, 600 kg/h, 1000 kg/h, 1500 kg/h, 2000 kg/h. Almost none of them will tell you what those numbers assume. That is the problem with capacity in this category - the figure is real, but it is conditional, and a buyer who treats it as absolute ends up either with a machine that cannot keep up at peak season or with a 1500 kg/h unit running at ten percent of its rating, burning power and disappointing the operator.
This guide sets out how to convert a real farm requirement into a defensible feed chopper capacity specification. It covers the daily-feed calculation, why moisture changes everything, what the single-phase ceiling actually is, how blade geometry interacts with throughput, and the derating factors that separate a catalogue number from a number you can rely on.
Start From the Herd, Not From the Machine
The correct sequence runs from animals to kilograms to kilowatts. Buyers who start from the machine work backwards from a price point and a capacity figure they found online, which is why so many installations end up mis-sized.
The calculation has four steps and takes about ten minutes:
- Count the animals and the type of feed. Daily chopping requirement depends on species, head count and how much of the ration is processed rather than grazed.
- Multiply to get a daily tonnage. Head count × approximate daily processed-feed allowance per head gives total kilograms per day of material that must pass through the machine.
- Divide by the hours actually available. This is the step buyers skip. A machine is not operated for twenty-four hours. If chopping happens once a day before feeding, the realistic operating window is one to two hours - sometimes less in peak season when other work competes.
- Apply a derating factor. The machine never delivers its rated figure on real material at real moisture. Apply a conservative factor, then choose the model above the result, not equal to it.
A worked example makes the logic concrete. Assume a small mixed operation needing 400 kg of chopped feed per day, chopping once per day in a one-hour window. The arithmetic requirement is 400 kg/h. Apply a 0.6 derating factor for wet material and intermittent loading, and the real requirement is roughly 670 kg/h. The correct choice is therefore a machine rated in the 700–1000 kg/h band - not a 400 kg/h machine, even though 400 is the nominal daily need.
That gap between the nominal figure and the correct specification is where most disappointing purchases originate. The simplest protection is to send the supplier the head count, the feed type and the operating window, and ask them to recommend a model - then compare their recommendation against your own derivation.
The Daily Feed Reference Table
The table below is a planning aid, not a feeding standard. Actual allowances vary by breed, age, productivity and whether the animal also grazes. Use it to establish an order of magnitude, then refine with the customer's own figures.
|
Operation profile |
Indicative daily chopped feed |
Realistic chopping window |
Implied kg/h requirement |
Motor band |
|
Smallholder, a few head + poultry, household use |
50–150 kg/day |
0.5–1.0 h |
100–300 kg/h |
1.1–1.5 kW single-phase |
|
Family farm, small dairy or mixed herd |
300–600 kg/day |
1.0–1.5 h |
400–900 kg/h |
1.5–2.2 kW single-phase |
|
Family workshop, feed prepared for others |
600–1200 kg/day |
2.0–3.0 h |
500–1200 kg/h |
2.2–3.0 kW single-phase |
|
Small commercial operation, multi-material |
1200–2500 kg/day |
3.0–4.0 h |
800–1500 kg/h |
3.0–4.0 kW (phase per site supply) |
|
Read the table as a sizing band, then buy at the top of it. A machine operating near its rated maximum is a machine operating near its reliability limit. Sizing to the upper end of the band buys operating margin, tolerance for wet material, and headroom for herd growth - usually at a modest price increment. |
Why Moisture Changes Your Number More Than Anything Else
Capacity figures in this category are normally quoted on favourable material: dry or low-moisture forage, cleanly presented, fed at a steady rate. Fresh green material and wet vegetable matter behave differently. Wet material is heavier per unit of usable feed, tends to bridge in the feed opening, loads the cutting chamber unevenly, and requires more power per kilogram cut. The result is a real throughput well below the rated figure - commonly twenty to forty percent lower, and worse in a machine with an undersized feed throat.
|
Material state |
Typical effect on throughput |
Practical consequence |
|
Dry forage, stalk, straw, hay |
Baseline rated figure |
Rated capacity is broadly achievable with steady feeding. |
|
Fresh green forage, cut grass |
Moderate reduction |
Expect a materially lower real figure; feed throat design matters more than motor size. |
|
Wet vegetable matter, root crops, silage |
Largest reduction |
Volume, not power, usually becomes the bottleneck; a shredder family better suited than a chopper. |
The practical instruction to a supplier is therefore not "what is the capacity" but "what is the capacity on this material, at this moisture, with this feed arrangement." A supplier who cannot answer that question in writing is quoting from a catalogue, not from experience - and the answer is the one most worth testing with a material sample before a container is committed.
Single-Phase Versus Three-Phase: The Real Ceiling
For South American agricultural markets, the dominant supply is 220V/50Hz, and the binding constraint on the farm is usually single-phase availability. This is not a technicality; it sets the ceiling on the largest machine a smallholder can actually run.
A single-phase 220V supply supports a compact feed chopper in the low-kilowatt band comfortably. As motor rating rises, single-phase starting current rises sharply, and the practical upper limit of what a rural domestic supply will tolerate arrives sooner than the nameplate suggests. Three-phase motors are cheaper per kilowatt, run more smoothly and start more gently - but they are useless at a site with no three-phase connection, and retrofitting a three-phase supply is a project, not a purchase.
The decision rule for the smallholder and family-workshop segment is therefore: choose the machine the site's supply can start, not the machine the catalogue recommends. In practice this means treating single-phase as the default for anything in the 1.1–3 kW band, and reserving three-phase for buyers who have confirmed a three-phase supply and whose throughput requirement genuinely exceeds the single-phase ceiling.
Two specification details materially affect whether a single-phase machine performs reliably in the field. First, copper-wound motors rather than aluminium: aluminium windings are cheaper and run hotter, and in a two-hour continuous peak-season run that difference shows up as premature failure. Second, cable and plug sized for the running current - an undersized supply cable produces voltage drop under load, which shows up as a machine that runs weakly or trips, and is frequently misdiagnosed as a motor fault.
Blade Count, Cutting Length and Throughput
Capacity is not only a function of motor power. The cutting arrangement determines how efficiently that power is converted into chopped feed, and it also determines whether the output is usable for the intended animal.
- Blade count. Manganese-steel blades in the four- to five-piece range are the common arrangement in compact choppers. More cutting edges per revolution generally mean a finer and more uniform cut for the same shaft speed, at the cost of higher torque demand.
- Cutting length adjustment. Adjustable cutting length, typically from roughly one to three centimetres depending on machine, is a genuine operating requirement rather than a luxury - different animals and different rations need different particle sizes, and the ability to adjust lets one machine serve a mixed operation.
- Blade condition. Throughput falls as blades dull. A distributor whose customers cannot obtain replacement blades will see repeat business collapse; blade and screen availability is a supply-chain commitment, not an accessory.
- Shaft speed and gearing. Higher shaft speed raises throughput but increases wear, noise and vibration. Machines built for longevity tend to run at moderate speed with a robust drive rather than at maximum RPM.
The useful specification question is not "how many blades" in isolation, but "what cutting length does this arrangement produce on my material, and what is the power draw at that setting." Uniform particle size matters nutritionally as well as visually: an inconsistent chop means animals sort the ration, and the fine fraction is wasted.
Derating Factors: Turning a Catalogue Number into a Planning Number
The gap between a rated figure and a delivered figure is the sum of several predictable losses. Planning with them explicit is what separates a specification that holds from one that disappoints.
|
Factor |
Typical effect |
How to mitigate |
|
Material moisture above the rating basis |
Significant reduction, worst on wet vegetable matter |
Specify against actual material; test with a sample. |
|
Intermittent manual feeding |
Moderate reduction |
Confirm feed throat design; consider a hopper or conveyor arrangement. |
|
Blade wear over a season |
Gradual reduction |
Stock replacement blades; specify blade material. |
|
Supply voltage drop under load |
Reduced effective power |
Correct cable gauge; confirm voltage tolerance. |
|
Peak-season continuous running |
Reliability risk rather than throughput loss |
Size to the upper end of the band; specify copper winding. |
Applying a single conservative derating factor to the nominal requirement captures most of this. A factor in the region of 0.6 to 0.7 against nominal daily need, where the machine will be fed manually with partly wet material, is a defensible planning assumption. Where material is dry, feeding is steady and the operating window is generous, a factor closer to 0.8 is reasonable.
Six Sizing Mistakes That Cost a Season
- Buying the rated figure as the delivered figure. The catalogue number is a best case; the delivered number is lower. Buy above the requirement, not at it.
- Ignoring the operating window. A daily tonnage divided by twenty-four hours produces a requirement far below what a one-hour chopping window actually demands.
- Specifying a machine the site cannot start. A three-phase machine at a site with no three-phase supply is scrap metal on arrival.
- Applying a dry-material capacity to wet material. The single most common cause of an under-capacity complaint.
- Treating capacity as independent of cut length. A finer cut at the same shaft speed reduces throughput; the two settings interact.
- Forgetting the consumables. A machine with no available blades stops working in the middle of the season, and the customer blames the machine.
What to Send a Supplier to Get an Accurate Recommendation
- A supplier can only size accurately against real inputs. Buyers who send these six items receive a specification that stands up; buyers who send "a feed chopper for 200 cows" receive an average of several guesses.
- Animal type and head count, and whether animals also graze.
- Primary material to be processed, with a description of its moisture state.
- Whether the material is mixed or changes seasonally.
- The realistic operating window per day, in hours.
- Available electrical supply on site: voltage, frequency and phase.
- Whether the output needs a specific particle size for the intended ration.
Sizing Across the Range: Chopper, Chaff Cutter, Silage Chopper, Shredder
The sizing logic above holds across the compact range, but the numbers move with the working family, and buyers who size a whole product mix on a single model's figures end up with a container that half-fits their market. A chaff cutter used for daily ration preparation is sized on the short pre-feeding window described earlier, because the whole day's feed is processed in one sitting. A silage chopper works against a different rhythm entirely: silage making is seasonal and concentrated, so the operating window is measured in days of intense use rather than minutes per day, and throughput matters more than duty-cycle tolerance. A mini forage chopper is deliberately sized below the daily requirement of the operation it serves, which makes it the right tool for the smallest farms and the wrong tool for anyone who has already outgrown hand feeding. A silage chopper and a hay chopper may share a platform but are set up for opposite ends of the moisture range, so the derating factor applied to each must differ.
For a wholesale feed chopper supplier quoting a mixed container, the sizing question sits one level up. The buyer no longer needs one correct machine; they need a container in which every specification is defensible for some segment of their market, which means the sizing spreadsheet becomes a range plan. Practical guidance for that is to hold one model in the smallholder band, one in the family-farm band and one combined machine for multi-material work, then add models only once a specification has demonstrated demand. Where a buyer wants their own branding on a specification, the MOQ moves with the order and should be confirmed in writing per model rather than assumed from a headline figure - and an OEM chaff cutter programme is priced and scheduled differently from a stock order, because production is committed against artwork rather than against inventory.
Frequently Asked Questions
What does kg/h actually mean on a feed chopper specification?
It is the mass of material the machine can process per hour under stated conditions - and the conditions matter as much as the number. A capacity figure quoted without reference to material type, moisture content and feeding method is a catalogue figure, not a planning figure. Always ask what the number assumes.
If my farm needs 400 kg per day, is a 400 kg/h machine enough?
Almost certainly not. Your real requirement is the daily need divided by the operating window, then derated for material and feeding. If chopping happens in a one-hour window and the material is wet, the correct specification is commonly around 700 kg/h or more.
Can I run a 3 kW feed chopper on single-phase 220V?
Generally yes, and that band is the practical sweet spot for the smallholder and family-workshop segment - provided the site's supply and cabling are adequate. Starting current rises with motor rating, so confirm the supply can start the machine, not merely run it.
Why does my machine deliver less than the rated capacity?
Almost always one of four causes: material wetter than the rating basis, intermittent manual feeding, dulled blades, or voltage drop from an undersized cable. Work through those four before concluding the machine is at fault.
Should I buy a chopper or a shredder for wet vegetable material?
For predominantly wet vegetable matter, a shredder family is generally the better fit; for long dry forage, a chopper. If your material mix changes through the year, a combined cutting and grinding processor is usually the more durable choice than forcing one machine to do both.
What is a realistic lead time for a customised feed chopper order?
Lead time varies by model, customisation and season, so it should be confirmed in writing per order rather than assumed from a general figure. Customised voltage, branding or packaging adds production time, and peak-season loading extends it further.
About the Supplier
Jiaxing Zenterest Import & Export Co., Ltd. is a China-based sourcing and export company established in 2017 in Jiaxing City, Zhejiang Province, working with a network of more than ten certified manufacturing partners across agricultural machinery and kitchen and bathroom appliances. We supply feed cutting machines, forage choppers, feed shredders and farm food processors, and we size machines against the buyer's actual material and operating window rather than against a catalogue average.
Our team has spent over a decade building and maintaining factory relationships in this category. The company operates with more than 100 staff and an annual turnover exceeding RMB 100 million, which lets us consolidate order volume across buyers to reach rate levels and production slots that individual buyers cannot access. Every partner factory is vetted before the first order and monitored afterwards.
Send us your head count, material, moisture state, operating window and site electrical supply, and we will return a model recommendation with a written throughput statement for your material.
Key Takeaways
- Size from the herd, not from the machine: head count → daily kilograms → divide by the real operating window → derate.
- The common derating factor for manual feeding with partly wet material is around 0.6 to 0.7 of nominal.
- Single-phase 220V/50Hz sets the practical ceiling for the smallholder segment; choose the machine the site can start.
- Moisture is the largest single driver of throughput loss - specify and test against actual material, not a favourable basis.
- Blade count and cut-length setting interact with throughput; a finer cut at the same shaft speed reduces output.
- Blade and screen availability is a supply-chain commitment that decides whether the customer comes back.
|
Send your sizing inputs and get a written recommendation Email: bonnie.wu@zenterestvent.com WhatsApp / Phone: +86 185 0573 0567 Jiaxing Zenterest Import & Export Co., Ltd. - Room 101-3, Building 46, Zhifu Center, Gaozhao Subdistrict, Xiuzhou District, Jiaxing City, Zhejiang, China |


